

At Edrisco Holding, we understand that high-quality production is only half the battle. The other half is ensuring that your order arrives in the exact state it left our facility. We employ rigorous packaging protocols tailored to the unique demands of our Agri-Food and Energy/Mineral portfolios.
Agri-Food Division: Preservation & Hygiene
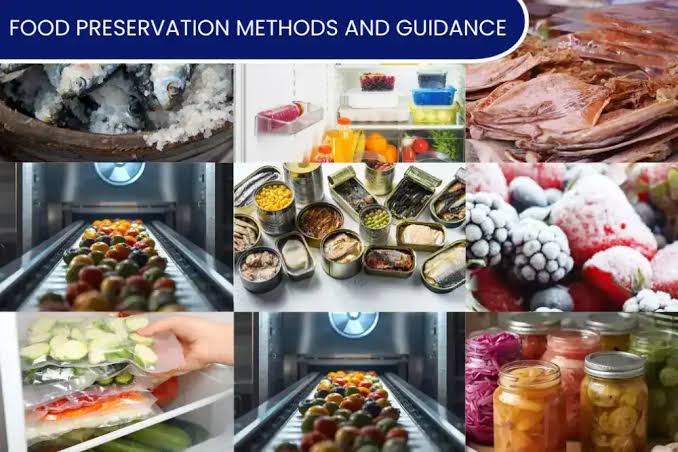
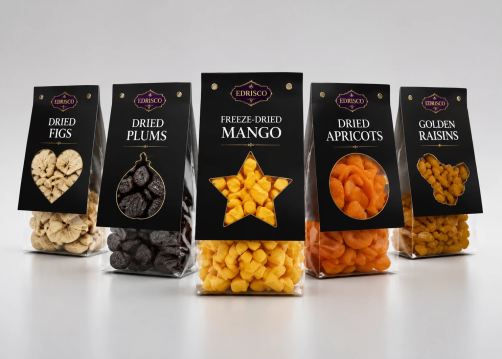
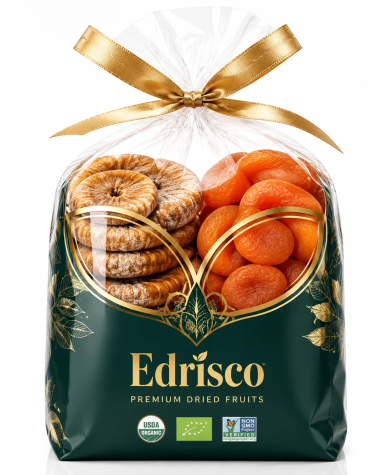
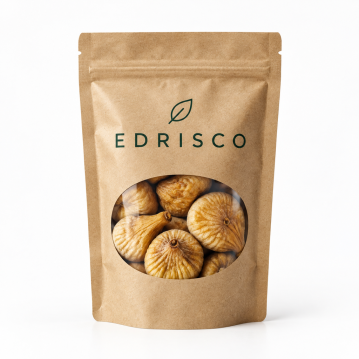
For our dried and freeze-dried products, we prioritize shelf-life stability and hygiene. Atmospheric Control: We utilize Food-Grade High-Barrier Films and Modified Atmosphere Packaging (MAP) techniques to prevent oxidation and moisture ingress. Sanitary Integrity: Every stage of our packaging process adheres to strict HACCP guidelines, ensuring that our products remain free from cross-contamination throughout the transit cycle. Scalable Solutions: From bulk vacuum-sealed liners for industrial processors to consumer-ready retail packaging, we tailor the material to your specific storage and shelf-life requirements.
Energy & Minerals Division: Durability & Safety
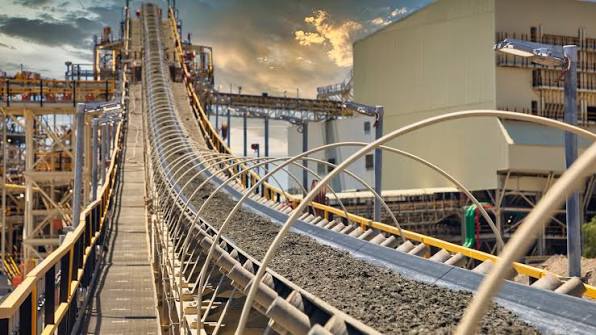
When moving industrial commodities and minerals, strength, stackability, and safety are paramount. Heavy-Duty Containment: We utilize FIBC (Jumbo Bags), reinforced multi-layer paper sacks, and UN-certified drums where required, designed to withstand high-pressure handling and long-haul maritime transport. Safety Compliance: All industrial packaging is marked with clear, international-standard handling instructions, and we ensure compliance with IMDG (International Maritime Dangerous Goods) codes where applicable. Moisture & Contamination Control: For sensitive minerals, we incorporate moisture-proof liners and anti-dust sealing, ensuring the chemical purity of your shipment is maintained from origin to port of destination.
Global Logistics Compliance (The Edrisco Standard)
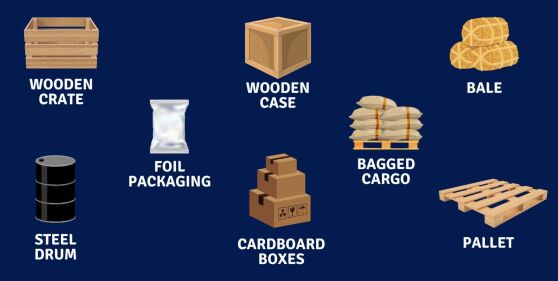
Regardless of the cargo type, we uphold universal logistics standards to ensure customs efficiency: ISPM 15 Compliance: All wooden pallets and dunnage used in our exports are heat-treated and certified according to the International Standards for Phytosanitary Measures (ISPM 15), ensuring zero-hassle clearance at international borders. Optimized Palletization: Our loading patterns are optimized for container space utilization, minimizing your “landed cost” by maximizing container volume without compromising safety. Traceability: Every pallet and master carton is labeled with clear, machine-readable barcodes and unique identifiers, allowing for real-time traceability within your warehouse management system.
Grow your business with our flexible packaging solutions designed for global expansion.
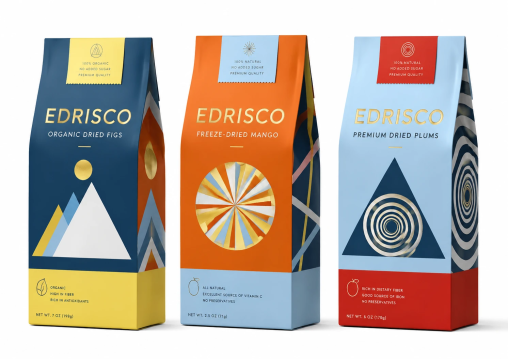
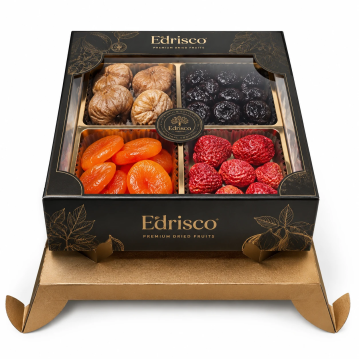
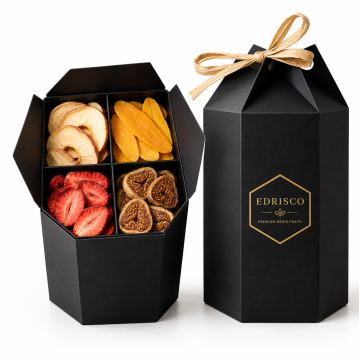
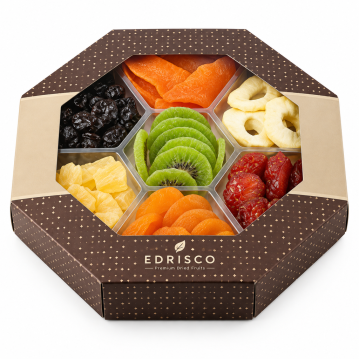
Private Labeling: Turn our premium products into your own branded line with ease.
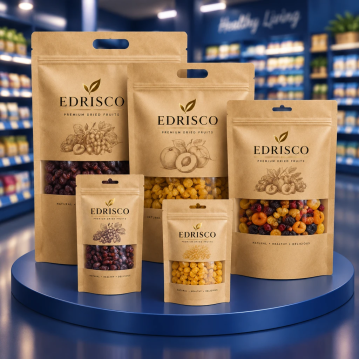
Custom Dimensions: From retail-ready small packs to industrial bulk sizes, we tailor packaging to fit your market’s needs.
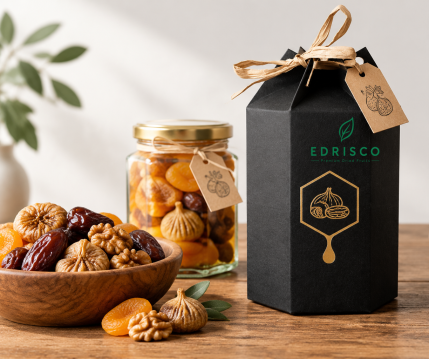
Branding Precision: High-quality, custom-printed packaging that makes your brand stand out on any shelf.
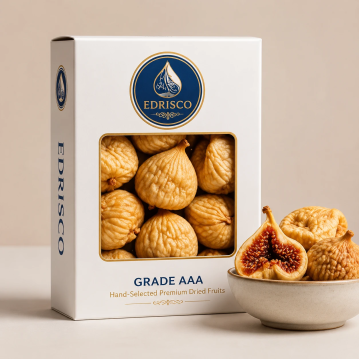
EBH101
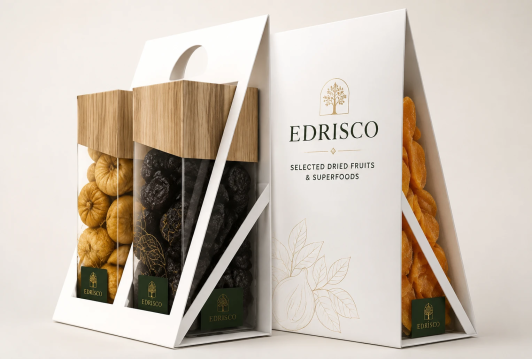
EBH102
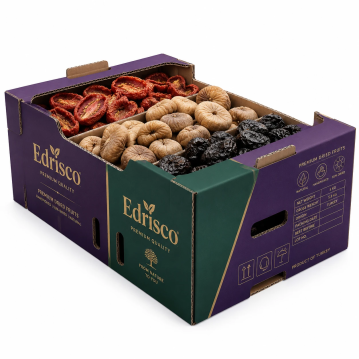
EBH103
EBH104
EBH105
EBH106
EBH107
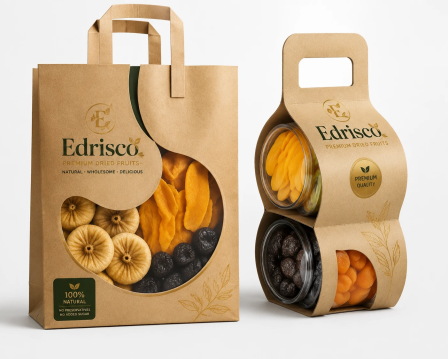
EBH108
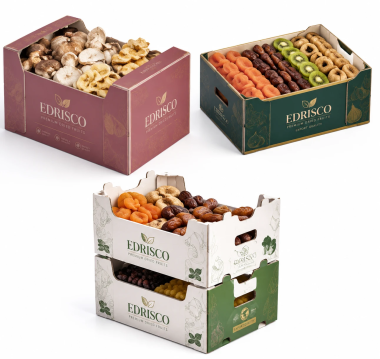
EBH109
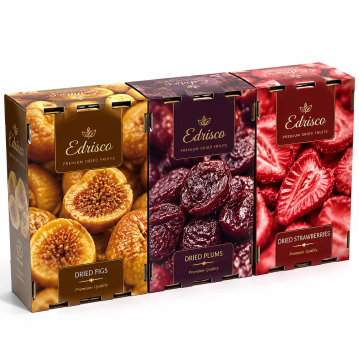
EBH110
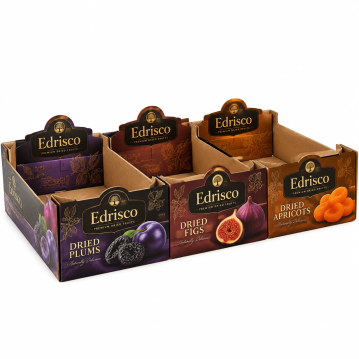
EBH111
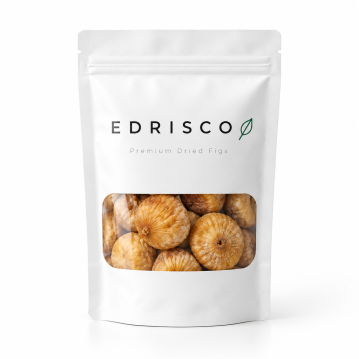
EBH112
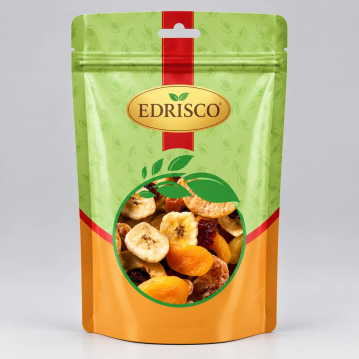
EBH113
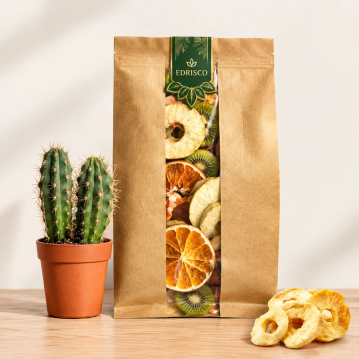
EBH114
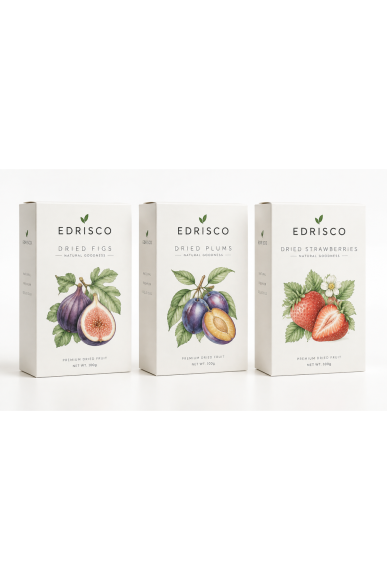
EBH115
EBH116
EBH117
EBH118
EBH119
EBH120